Choose the Process From the Part You Need
Laser cutting and CNC routing solve overlapping fabrication problems, but their useful differences appear in a specific part rather than a universal ranking. A flat acrylic display, a wooden recess and an interlocking enclosure ask different questions about material compatibility, internal corners, depth, workholding and finishing. This guide compares those three decisions, then shows how to request a representative test and a complete quotation. It distinguishes suitable CO2 processing from other laser sources and treats router capability as machine-specific too. Start with a dimensioned requirement and the actual stock. The goal is to select a supported process that delivers the finished result, with its setup and limitations visible before production begins.
A: A suitable CNC router can create a controlled pocket, but stock, tool access, workholding and the required depth must be established.
A: A round cutter leaves a radius. Redesign the mating geometry, use appropriate relief, or choose a suitable additional process.
A: No. Material is removed across a finite width that can affect dimensions and fitted joints.
A: No. The actual wavelength and machine capability matter; clear acrylic is a key limitation for blue-diode through-cutting.
A: Cutting forces and final separation can move parts unless the documented workholding strategy controls them.
A: No. Include usable yield, file work, setup, consumables, machine time, cleanup and the necessary operating controls.
A: It can suit a project with complementary flat outlines and machined features, provided material compatibility and alignment are planned.
A: No. Fit depends on the actual stock, kerf, compensation and finishing; test a representative coupon.
A: State the stock, geometry, tolerances, quantity, finishing, inspection and any unresolved assumptions that affect price or feasibility.
A: Bring a dimensioned design and material requirements to a trained workshop or service, then compare suitable sample processes and complete costs.
Describe the Required Geometry Before Comparing Machines
Begin with a dimensioned part and its intended material, quantity and service. A flat outline, a shallow pocket and a three-dimensional surface ask different things of the process. State which dimensions must fit another component and which edges are only decorative. Include whether a darkened edge, visible cutter marks or further finishing would be acceptable. This turns a broad machine comparison into a specific fabrication decision.
Keep the scope of the equipment explicit. Here, laser means a suitable enclosed system operating within its documented material capability, with CO2 used for the acrylic example. Router means an appropriately equipped CNC routing system with the required stock, tooling, workholding and operating controls. A blue-diode engraver and a fiber marker cannot inherit every CO2 cutting claim, and a small hobby router cannot inherit every industrial machining capability. Compare actual supported processes rather than choosing from two general labels.
Check Material Eligibility Before Edge Quality
A process that cannot appropriately handle the stock is removed before comparing speed or appearance. For laser work, identify the polymer, coating, adhesive layers and thickness, then obtain approval for the actual machine. Clear acrylic is a useful distinction: suitable CO2 equipment can cut it, while a blue-diode setup generally cannot do the same through-cut. A surface-marking workaround is not proof of equivalent cutting capability. Unknown plastic should be identified or rejected rather than tested by burning.
For routing, check the actual stock and cutter combination, machine capacity and required workholding. Material behavior can affect chip formation, heat, surface quality and tool life. An approved wood operation does not establish a suitable metal-cutting process on the same machine. Keep the stock’s fabrication information beside the machine instructions. Do not choose a cutter solely because its diameter fits the drawing.
Both processes need their own exposure and operating arrangements. Laser fumes require suitable extraction or filtration, while routing produces chips and potentially fine dust needing appropriate control. Guards, enclosures, access restrictions and operator training remain part of the comparison. Never leave an operating laser unattended, and follow its material restrictions, including manufacturer prohibitions on PVC or vinyl. A small desktop footprint does not make either complete installation simple.
Read Kerf and Cutter Radius Correctly
A laser removes a finite width of material, called kerf, rather than following a zero-width line. A round router cutter also removes a finite path and leaves a radius in an ordinary internal corner. A mating square tab may therefore need changed geometry or appropriate relief in a routed opening. The visible stroke width in a design file is not automatically the machine’s cut width. Use a representative sample and the actual compensation strategy when fit matters. Aalto University’s laser-design guidance explains the need to consider real paths and kerf rather than only the screen drawing.
Decision One: Make a Flat Acrylic Display Shape
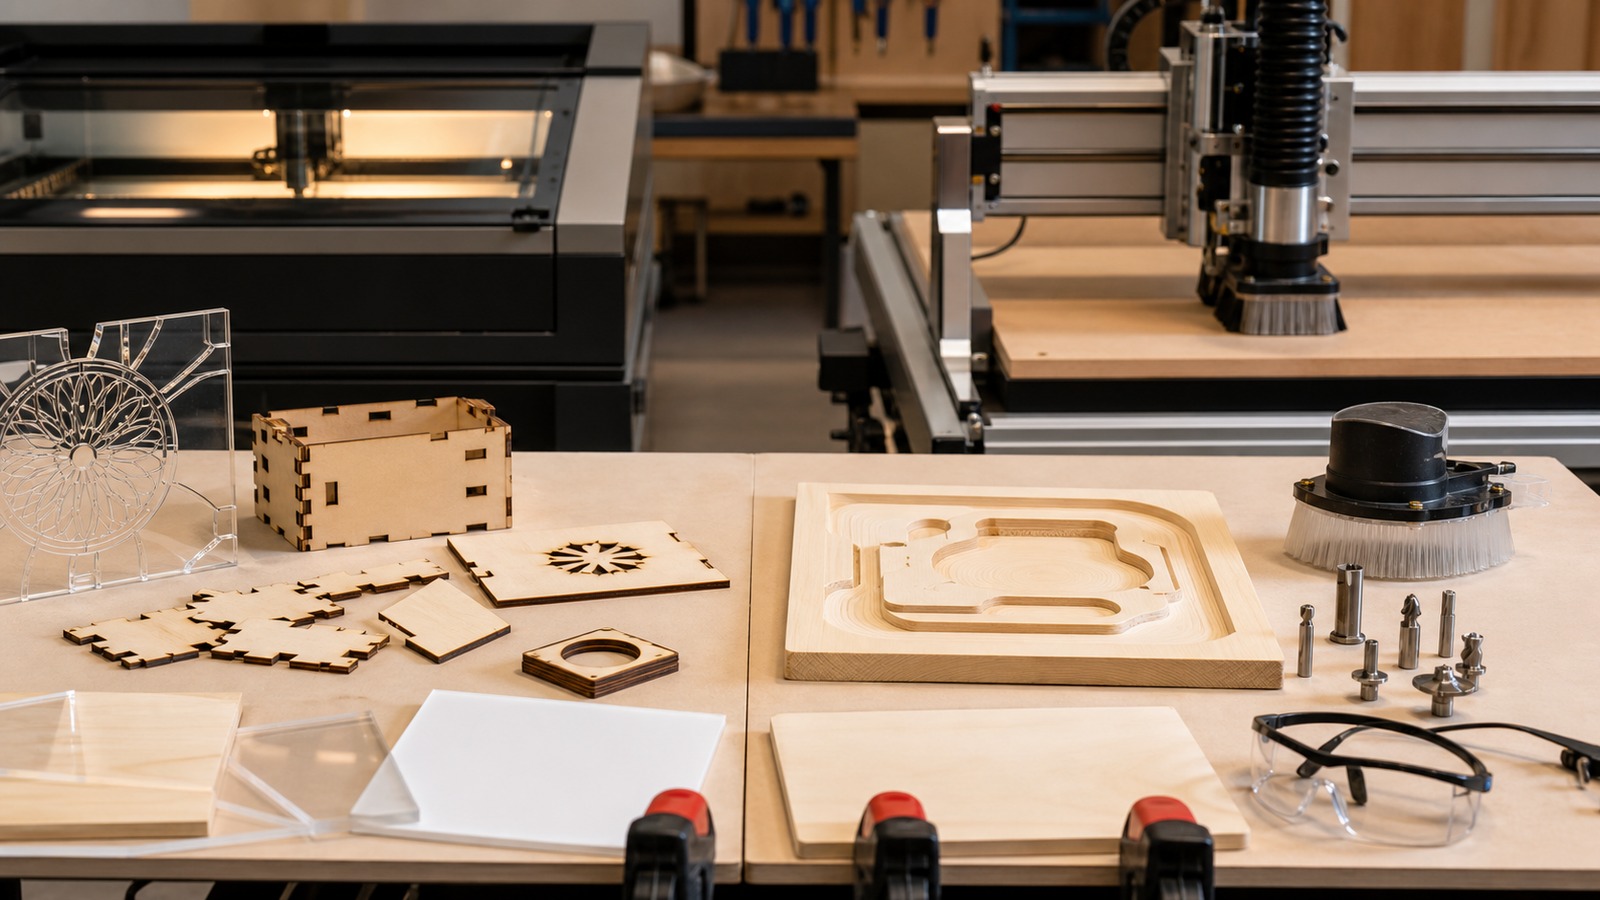
Suppose the project is a modest flat display shape in identified clear acrylic, with an outside outline and a small hanging hole. Ask an appropriately equipped workshop whether its CO2 machine supports the actual sheet and thickness. If it does, a laser can be a candidate for producing those flat features without a rotating cutter’s cutting forces. The part still needs suitable support, focus, operation mapping and supervised processing. Inspect a sample edge rather than assuming every acrylic product will produce the same finish.
A router may also be a candidate if it supports that stock, thickness and geometry with appropriate tooling and retention. The small hole, internal details and required edge quality can change the tool and finishing plan. Compare the finished part, not a clean laser sample against an unfinished routed edge. If both meet the requirement, setup, quantity and available service may decide the practical choice. If the only available laser is an incompatible blue-diode system, the material capability has already decided that route’s eligibility.
For a dimensioned comparison sample, draw an illustrative 180 by 120 millimeter display with two 8 millimeter holes, their centers 25 millimeters inward from the upper corners. Give both services the same drawing and the same identified sheet requirement. Ask them to report the delivered outside dimensions, hole sizes and any edge-finishing stage rather than comparing unmatched demonstration photographs. These dimensions define a small geometry exercise, not a rated suspension design. The proposed attachment, stock thickness and service still need their own assessment. If one quote changes the hole or substitutes another material, resolve that difference before calling the two prices comparable.
Decision Two: Recess Hardware Into a Wooden Part
Now consider a wooden component requiring a flat-bottomed pocket to a specified depth while retaining material beneath it. A suitable CNC router can be a practical candidate because its supported toolpath controls the machined cavity as well as the perimeter. Check stock thickness, cutter access, corner radius, fixture and the actual depth reference. Laser engraving can remove material in some supported applications, but that does not automatically establish the required pocket depth, flatness or dimensional control. Choose from evidence about this cavity rather than claiming either technology owns every possible depth feature.
Decision Three: Build a Small Sheet Assembly
A small enclosure made from flat interlocking panels can be feasible through either process, depending on the stock and geometry. Start by measuring actual sheet thickness and deciding how the joints should behave. A glued slip fit, a removable sliding cover and a friction-held model have different clearance needs. Do not apply one universal slot allowance merely because a previous box assembled successfully. Include the intended coating or finishing effect in the fit trial.
For laser-cut panels, verify the machine’s actual kerf and whether compensation is applied in the drawing or control software. For routed panels, account for the cutter’s internal-corner geometry and retention near final separation. A tab designed as a perfectly sharp rectangular corner can clash with a rounded pocket unless the design provides the appropriate relief or mating shape. Make a small joint coupon before cutting every wall. This inexpensive part answers a more useful question than a large decorative sample with no fitted features.
A combined process can be sensible when different features justify it. A flat face panel might be laser-cut while a suitable router makes a separate recessed base. Plan shared dimensions and alignment references instead of assuming the two files will meet automatically. Check material and joining compatibility for the whole assembly. Combining machines is useful when it solves defined requirements, not when it adds an unnecessary second setup.
Compare Workholding and Operation Order
Routing applies cutting forces that make workholding central to the job. Clamps, fixtures or other approved retention must control the stock while remaining clear of the cutter and its travel. Small parts require particular attention as the last material connection disappears. The chosen method can affect waste margins and the usable stock area. Previewing a toolpath cannot prove the actual fixture is secure or clear of the machine.
Laser work also needs appropriate support and an order that suits the part. Internal features or engraving may need to be completed before an outside cut releases a piece, under the actual workflow. Remove duplicate paths and verify imported dimensions and operation assignments before sending the job. Colors and line attributes have machine-specific meanings, so a familiar red outline does not establish a universal cutting instruction. Keep the operator’s accepted file setup with the project.
Compare Complete Time and Cost
Ask each service to identify stock, usable yield, file preparation, setup, machine time, consumables, inspection and finishing. A fast visible cut can still require substantial preparation or cleanup. Routing may involve tool changes or a second setup, while laser engraving can add considerable processing time beyond the outline. Include rejected trials and the work required to achieve the specified edge. Compare equivalent finished deliverables with the same quantity and tolerance assumptions. A lower quoted machine rate is not evidence of a lower completed-project cost.
Use a Decision Table With Clear Limits
The table summarizes the worked examples without selecting a universal winner. Each candidate remains conditional on the actual machine, approved stock and complete setup. Add the exact local equipment or service to your own version before requesting a sample or quote. If an essential capability is unverified, leave that candidate unresolved rather than awarding it an optimistic score. Material eligibility and operating requirements come before convenience.
| Required result | Laser route to investigate | Router route to investigate |
|---|---|---|
| Flat clear-acrylic outline | Suitable CO2 process with approved stock, thickness and edge evidence. | Compatible cutter and retention, with required edge finishing included. |
| Controlled wooden recess | Only if a supported process demonstrates the required cavity dimensions and surface. | Suitable pocket toolpath, depth reference, cutter access and fixture. |
| Interlocking sheet enclosure | Measured kerf, compensation and a representative finished joint coupon. | Measured stock, internal-radius accommodation and controlled part retention. |
Keep service consequences beside the geometry. A decorative sign, a removable cover and a load-bearing bracket need different evidence before use. Neither a clean laser edge nor a precise-looking router finish certifies strength, fire behavior or food-contact suitability. Those requirements belong to the material and complete design assessment. Avoid upgrading an informal sample into a demanding application without the appropriate engineering or product evidence.
Validate One Representative Feature Before Production
Ask for a test that contains the feature most likely to decide the process. For the display, that might include the actual hole and outside curve; for the recessed part, the cavity and corner; for the enclosure, a mating joint. Use matching stock, thickness and finishing conditions. Measure or inspect against the written requirement rather than only asking which sample looks nicer. Keep the test’s limitations explicit if it does not represent the whole production setup.
When a sample fails, identify the cause before switching technologies. An incorrectly imported scale is a file problem, a damaged edge may involve the process or tool, and a loose assembly may involve dimensions or compensation. Preserve the failed sample and its settings where the workshop permits. Change the relevant cause and repeat the meaningful check. A second machine cannot repair a requirement that was never defined.
Keep the accepted drawing, stock identity, process, finish and inspection result together. Revisit the decision if the quantity, thickness, geometry or service changes. Manufacturer machine manuals, material fabrication information and the workshop’s operating procedure provide the specific boundaries around this comparison. The useful choice is the supported process that produces the required finished object predictably. Select it once the evidence is sufficient, then proceed with one coherent fabrication plan.